
It can be normal and it can be a problem, and the difference is whether anyone wrote anything down after batch one. Colour or speed that drifts between batches is almost never deliberate — it is what happens when the chip, the colour sample and the batch record were approved as a one-time event instead of locked in as the specification.
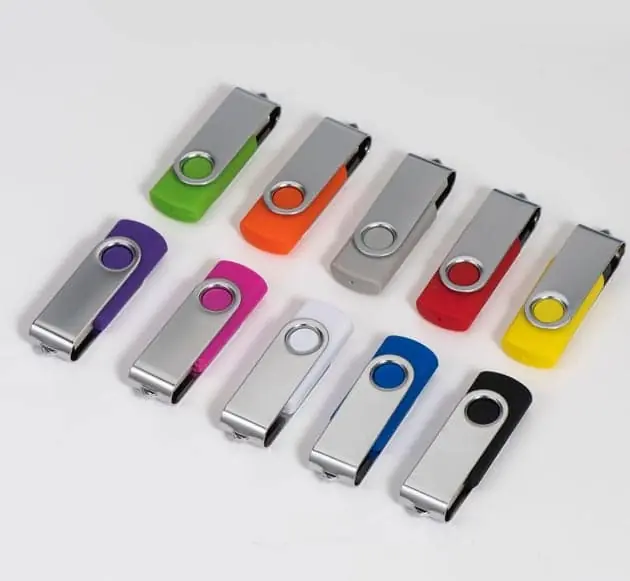
A second or third batch that looks or performs different from the first is common, and sometimes acceptable — but it is never acceptable if nobody wrote the first batch down as the standard. Treat the first batch as an approval event, not a one-time pass: keep a retained sample, approve a physical colour sample rather than a Pantone number, record the exact NAND and controller on the batch report, and require every later batch to be compared against the retained one. Batch-to-batch drift is cheap to prevent at order one and expensive to discover at batch three.
The short answer
It can be normal, and it can be a real problem. The difference between the two is almost never the supplier’s honesty — it’s whether anyone wrote the first batch down as the standard or just approved it as a one-time pass.
If batch one was approved and then everyone moved on, batch three drifting is almost inevitable. If batch one was recorded — sample kept, parts named, colour approved against a physical chip — then batch three is something you can measure against it.
So the question isn’t really “is drift normal.” It’s “did I lock the first batch in as the spec, or did I just say yes once?”
Why drift happens (and why it’s rarely sabotage)
Colour and performance don’t usually change because someone decided to cut a corner. They change because nothing was pinned.
- Moulded colour shifts with pigment dosing from shot to shot. Tiny on its own, visible across two runs.
- Component allocation moves between production slots. The NAND and controller available in March aren’t always the ones available in June.
- A print plate wears; a screen-print jig drifts; a fixture loosens.
Each of these is small. They add up. And without a retained first-batch sample, you can’t tell a normal few-percent shift from a quiet change someone made — so you argue instead of measure.
The one decision that prevents it
Treat the first batch as an approval event, not a pass.
When batch one arrives and looks right, most buyers say “great” and move on. That’s the mistake. The right move is to turn batch one into the reference everything else is judged against:
| Keep | Why |
|---|---|
| One unopened drive | Colour and finish reference you can put next to later batches |
| The signed colour sample | The physical chip you approved, not the Pantone number |
| The batch test report | Names the exact NAND and controller used |
Those three turn “this looks different” into a yes-or-no measurement. Without them, every reorder starts from memory — and memory is exactly where consistency goes to die.
Colour: why your Pantone number isn’t enough
This is the one buyers trip on most. You specify PMS 226C, the supplier says “matched,” and batch three is visibly off.
The reason isn’t carelessness. A Pantone reference is printed on coated paper. Your drive is a moulded, textured material. The same formula reads differently in ABS, in soft PVC and in painted metal — and it reads differently shot to shot within one material.
What actually holds the colour is a physical sample you approved in the real material and finish, kept by both sides. The Pantone number is the target. The approved sample is the specification.
A scenario buyers recognise: a brand runs a pink drive. Batch one is right. Batch three, from a different production slot, comes back a shade off. The Pantone was identical on the order both times. What changed was that nobody retained the batch-one chip, so “off” became a feeling instead of a measurement.
Speed: when capacity passes but behaviour doesn’t
A subtler version: batch three’s capacity tests fine, but it feels slower under a big transfer. Capacity-only incoming checks miss this completely, because capacity is the same.
What changed is almost certainly the controller or NAND grade, or the same parts built to a different firmware. All of those pass a capacity write-and-read-back. None of them behave the same under sustained load.
The batch report that names the parts is what reveals it, and a fixed-BOM clause is what gives you a remedy. Speed drift that passes a capacity test is the classic silent swap — and it’s the reason a capacity-only check is not a quality check.
A scenario: batch three, two years of reorder
Picture a buyer running a branded drive as a recurring promo.
- Batch one: approved on a video call. “Looks great, ship the rest.”
- Batch two: fine, nobody notices.
- Batch three: the end customer says “these look like fakes, the pink’s wrong and a couple felt slow.”
The supplier didn’t necessarily do anything wrong. The buyer just never wrote batch one down. There’s no retained sample, no recorded part numbers, no comparison standard. “Looks like fakes” is now an opinion against an opinion.
With the three kept items, the same complaint becomes: “batch three’s colour sample is 4 shades from the retained batch-one chip, and the controller on the report is model Y, not the X in your PO.” That’s not a feeling. That’s a finding.
The questions to ask before reorder one
- Did I keep a retained sample from the approved batch?
- Did I approve a physical colour chip, not just a Pantone number?
- Is the exact NAND and controller recorded on the batch report?
- Does my PO require later batches to be compared against the retained sample?
- Do I have a stated tolerance, or just “should match”?
None of this needs a big quality system. It needs three things kept and one line in the PO. The buyers who skip it are the ones writing “why is batch three different” six months later — which is a question that’s much easier to prevent than to answer.
Frequently asked questions
Is some variation between batches inevitable?
Some, yes. Moulded colour shifts slightly with pigment dosing from shot to shot; component allocation moves between production runs; a screen-print plate wears. None of these is large on its own. The problem is that they add up, and without a retained first-batch sample to compare against, you can't tell a normal few-percent shift from a supplier who quietly changed something. A retained sample turns 'looks different' into a measurable yes or no.
Why does my colour drift even though I gave a Pantone number?
Because a Pantone reference is printed on coated paper and your drive is a moulded, textured material. The same formula reads differently in ABS, soft PVC and painted metal, and it reads differently shot to shot. What actually holds the colour is a physical sample you approved in the real material and finish, kept by both sides. The Pantone number is the target; the approved sample is the specification.
What should I keep from the first batch?
Three things: one unopened drive as a colour and finish reference, the signed-off colour sample, and the batch test report that names the exact NAND and controller used. Those three let you answer 'is batch three within tolerance of batch one?' with a measurement instead of an argument. Without them, every reorder starts from memory, and memory is where consistency goes to die.
The speed dropped on a later batch but the capacity is right. What happened?
Almost certainly a different controller or NAND grade, or the same parts built to a different firmware. Capacity tests pass either way, which is why a capacity-only incoming check misses it. The batch report naming the parts is what reveals it — and a fixed-BOM clause is what gives you a remedy. Speed drift that passes a capacity test is the classic silent swap.
How do I tell a supplier the later batch is off without accusing them?
Send the retained first-batch sample next to the new unit and a measured comparison — colour difference if you can, or the two batch reports side by side. 'Batch three's controller reads as model Y, batch one was model X, per the PO — can you confirm why?' is a factual question, not an accusation, and it gets a factual answer. The retained sample is what makes the question possible.
Should I expect to pay more for guaranteed consistency?
Not usually as a separate line. Consistency mostly costs the supplier discipline — recording the parts, keeping the sample, comparing each batch. What can cost more is a tighter tolerance or a custom colour that needs its own retained standard. Ask upfront what they keep between batches; a supplier with a real retained-sample process will describe it quickly, and one who hesitates is telling you they don't.